Advanced Manufacturing & Technology
Advanced manufacturing facilities continue to increase in complexity, regulation, and equipment integration. Industries such as semiconductors, biotechnology, and aerospace depend on tightly controlled environments and highly coordinated process systems to meet performance, quality, and reliability requirements.
These facilities must support rapid technology cycles while remaining adaptable to retooling, expansion, and evolving regulatory standards. Early decisions related to process systems, utilities, and equipment integration have lasting impacts on uptime, operational efficiency, and long-term capital planning.
Farnsworth Group brings decades of experience designing process-intensive and controlled environments where manufacturing tools, building systems, and infrastructure must function as an integrated system. Our work spans planning, design, construction support, and facility upgrades across a wide range of advanced manufacturing environments.
We focus on aligning technical requirements with operational realities. That includes understanding how equipment is installed, supported, maintained, and expanded over time, and how those needs translate into facility layout, utility distribution, redundancy, and safety strategies.
Our teams collaborate closely with owners, contractors, and equipment vendors to integrate complex requirements into coordinated design solutions. The result is facilities that perform reliably, adapt efficiently, and support long-term operational goals.
Markets
- Advanced Research Facilities
- Aerospace
- Biotechnology Manufacturing
- Data Centers
- Industrial
- Life Sciences
- Manufacturing
- Pharmaceutical Facilities
- Semiconductor
Areas of Expertise
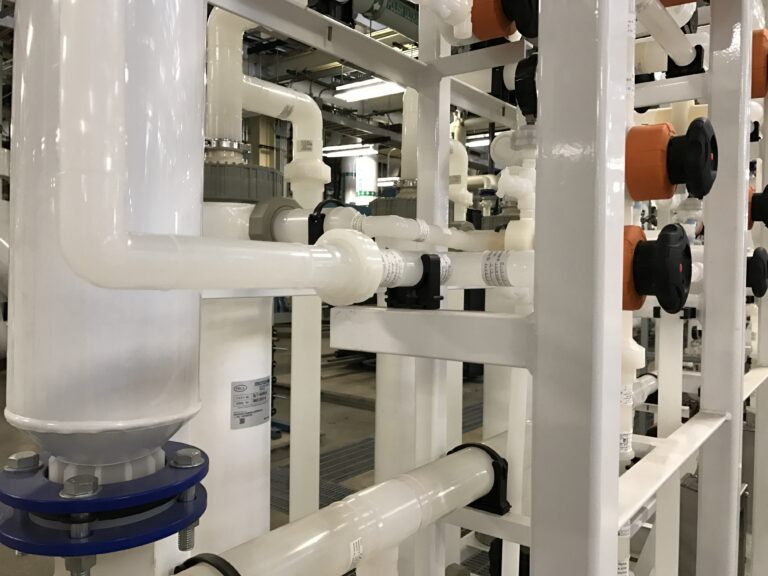
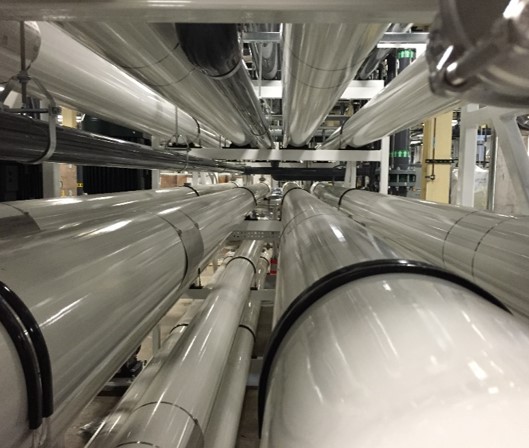
Areas of Expertise Our Advanced Manufacturing & Technology practice supports facilities where precision, control, and system reliability are critical. – Fab and cleanroom facilities, including manufacturing environments and SCIFs – Laboratory environments for research, biotechnology, formulation, and sterile operations – Process systems including ultrapure water, chemicals, specialty gases, and water management – Process mechanical systems supporting cooling, steam, compressed air, and utility infrastructure – Instrumentation and controls for monitoring and system integration – Telecommunications and data infrastructure supporting equipment and operations – Life safety and fire protection systems integrated with process hazards and code requirements
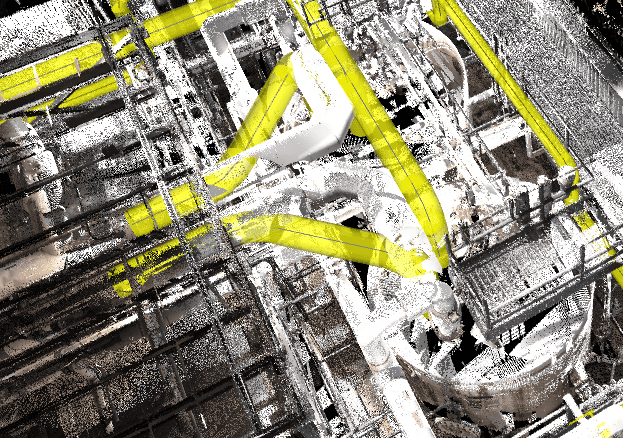
AMT Process Team Differentiators
Our differentiation is grounded in technical depth and execution, not marketing claims. – Ultrapure water distribution loop design and system analysis informed by operational demand and future capacity planning – Specialty chemical and gas expertise, including SDS review, chemical classification, MAQ calculations, and occupancy determination – Development of Hazardous Materials Inventory Statements and Hazardous Materials Management Plans aligned with regulatory requirements – Preparation of specialty process design packages and equipment vendor RFPs to support procurement and coordination – Hydraulic modeling and pipe stress analysis to support system reliability and long-term performance